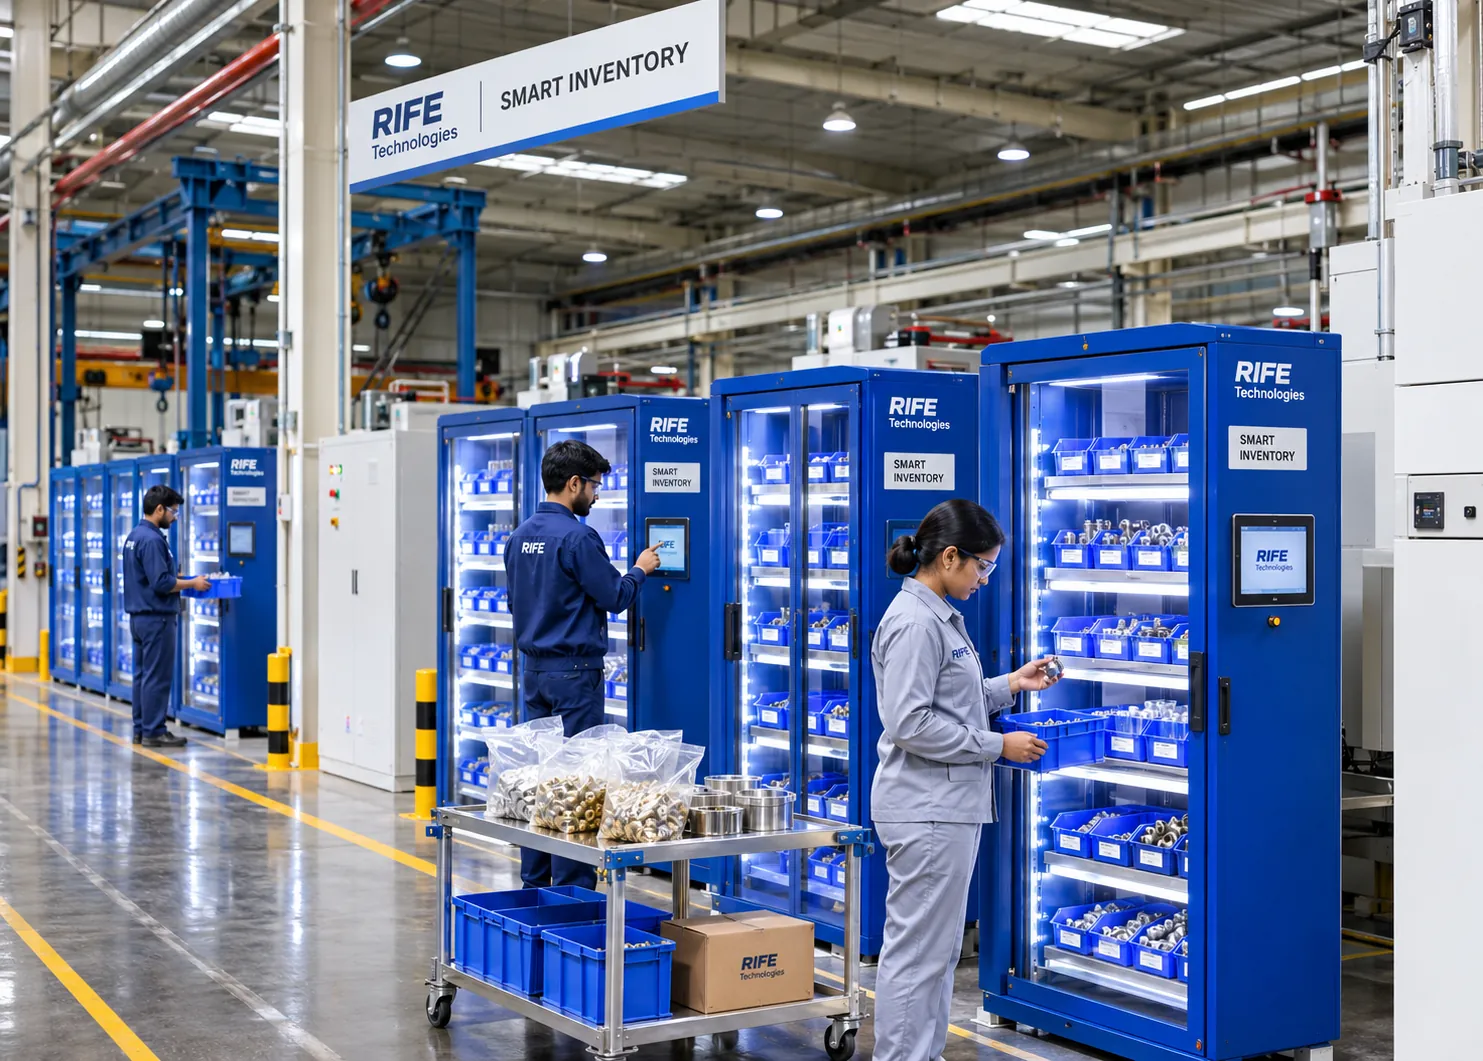
How smart shelves, monitored Kanban bins and controlled tool storage support manufacturing lines, stock visibility and timely replenishment.
Why manufacturing lines need stock visibility at the point of use
An assembly line may have adequate total stock in the warehouse but no screws at the workstation that needs them. The operator then leaves the station, asks for an urgent refill or waits for a material handler. A smart shelf targets that local gap between book inventory and the actual quantity sitting beside the work. It can monitor known parts at their assigned storage positions and make low-stock locations visible before the bin runs empty.
The most valuable starting point is not the most technologically interesting rack. It is a component whose absence regularly causes a delay. Identify the line, the part family, how often it is consumed and how long it takes to replenish. A timely stock signal becomes useful when someone on the replenishment team owns the next action.
Select line-side fasteners and consumables as a pilot
Fasteners, washers, clips and standardized components are common candidates for weight-based monitoring because they are often kept in dedicated bins and picked repeatedly. Their relatively consistent unit weight allows a properly calibrated sensor to calculate a remaining item quantity. Pilot selection should include representative full-bin loads, normal pick quantities, expected refill sizes and actual packaging.
A bin of highly variable mixed parts is different. If bolts and washers share a measuring position, a weight change alone cannot identify which one moved. Use separate compartments or another identification method. A practical pilot should not avoid challenging real handling conditions, but it should begin with items for which an interpretable measurement is possible and the production benefit is clear.
Turn weighing positions into a digital Kanban signal
Physical Kanban cards and two-bin layouts help factories replenish without complicated transactions, but they depend on a person moving the card or container at the appropriate time. In a monitored bin, a calibrated count is compared with an item-specific reorder point. When stock reaches that point, the software can flag the bin for replenishment even if nobody has noticed an empty container.
The replenishment rule must still reflect production reality. A fastener used quickly during one shift may need a higher threshold than a less frequently used spare. Include transport time, stores rounds, container capacity and the line's normal demand. The goal is to provide enough warning for material handlers to refill predictably rather than produce constant alerts that people ignore.
Design shelves around operators and bins
A sensor cannot rescue a poor mechanical layout. The bin must sit on the intended weighing surface with a stable load path, while operators should be able to remove parts without straining or moving unrelated containers. Shelf spacing, labels, dividers, cable routes and the visibility of status indicators should follow the normal picking routine. A shelf used at waist height in an assembly cell has different design needs from a high warehouse rack.
Use drawings or measured photographs of the current line-side station before selecting a new frame. Existing steel racks may be suitable for sensor retrofits if their support geometry is stable. Decide where electronics can be serviced, how cable protection will work and what happens during cleaning or shelf relocation. Operational acceptance should include user comfort as well as reading quality.
Calibrate the count for the smallest meaningful pick
The full bin includes the container tare and the weight of all stock. A typical component withdrawal creates only a fraction of that loaded mass. The system must tolerate the maximum weight while detecting the smallest change that matters to the replenishment decision. That tradeoff defines sensor selection and how many independent measuring zones are appropriate.
Unit-weight calibration should use representative parts, including any differences between supply batches and packaging. Test the count at full, partially used and nearly empty positions. Repeat ordinary picks and refills while adjacent stations operate. The finished shelf assembly may behave differently from the sensor data sheet, especially around vibration and loading changes. Agree acceptance criteria for actual production conditions.
Connect inventory changes to stores and purchasing
A dashboard should show more than a number. It should connect each shortage to a site, line, rack, shelf, part number and designated refill action. Stores staff can review which positions require attention and plan one efficient replenishment round instead of responding to multiple separate calls. Purchasing may review overall consumption and reorder needs across departments.
Real-time stock visibility does not automatically imply a working ERP purchase-order integration. If the customer wants a WMS or ERP connection, define the interface, item identifiers, exchange frequency and exception handling in the project. A simple validated dashboard with actionable low-stock lists can be more valuable than a broad integration claim that has not been demonstrated.
Add controlled tool storage where the process needs it
Production lines also consume drills, cutting inserts, bits and other tooling that may need user accountability. Open weighing shelves can monitor remaining stock, but they do not inherently know who took it. An RFID card or PIN-controlled cabinet can identify the employee opening the door. When properly combined with separate weighing positions, quantity changes during that controlled session can be linked to the authenticated user.
Returnable tools need another process. A torque wrench or specialized tool is normally checked out and returned as an identified item, rather than consumed as a quantity. A smart tool crib can combine the cabinet, weighing drawers and issue/return records. Designing those workflows separately prevents stock dashboards from confusing consumed parts with tools that are still expected back.
Plan for vibration, movement and exceptions
Manufacturing environments are active. Adjacent machinery vibrates, operators rest items on shelves, forklifts travel nearby and bins get shifted during replenishment. A robust monitoring configuration needs a mechanical assembly and signal-processing approach that handles normal disturbances. An unexpected weight change should not automatically be interpreted as a completed part withdrawal.
During the pilot, deliberately reproduce foreseeable exceptions: an operator lifts a bin, replaces it slightly differently, adds the wrong part, or changes the container. Record what the system displays and how the operator corrects the stock record. A clear exception procedure is part of the deployment, just as calibration and wiring are. Not every unusual event can be resolved without some manual confirmation.
Measure usefulness with production and stores staff
The value of a smart shelf project is reflected in daily work, not in an arbitrary headline percentage. During the trial, record how often staff manually inspect bins, when low-stock alerts occur, how quickly refills are completed and whether the monitored positions suffer avoidable shortages. Compare against a baseline period with similar materials and working conditions.
Involve the operators who pick the components and the stores workers who refill them. They will identify impractical shelf heights, labels that are difficult to read and thresholds that do not match the material route. Use their observations to improve the mechanical arrangement and software workflow. A counted bin is valuable only if people trust it and can act on its signals.
Roll out across lines with a consistent location structure
Once a pilot is accepted, extend the architecture by production cell, material family or stores zone. Use consistent location labels, item identifiers, calibration procedures and user roles. The team should know who can change an item's unit weight, who reviews exceptions and who maintains sensor hardware after a rack modification. Changes to production layouts may require remapping or recalibration.
A factory may ultimately use open shelves for standard fasteners, locked weighing drawers for costly consumables, a smart tool crib for reusable tooling and dedicated platforms for heavy components. Those formats can contribute to one coherent inventory view where the chosen software modules support them. The deployment plan should grow from proven use cases, not from pressure to automate every item at once.
Prepare a useful specification for suppliers and engineering
To request a practical design, provide the item list, nominal unit weights, packaging, maximum full-bin mass, bin dimensions, rack drawings, number of monitored positions and normal withdrawal pattern. Identify the access requirements, internet or network constraints and the stores or ERP reporting needed. Include photographs showing available clearance and likely cable routing.
Ask the supplier to distinguish available equipment, configurable options and features requiring further engineering validation. Agree how the installation will be tested and what evidence will demonstrate successful counting. A structured specification reduces misunderstandings about rated loads, capacity, accuracy and software integrations. It also helps procurement compare the proposed solution on operational fitness rather than simply the number of sensors.
Key considerations
- Choose line-side materials whose absence frequently disrupts production.
- Use known items in dedicated weighing positions and validate counts under real machine-floor conditions.
- Link low-stock signals to defined stores routes and accountable refill actions.
- Expand by workcell or item family after the pilot meets practical acceptance criteria.